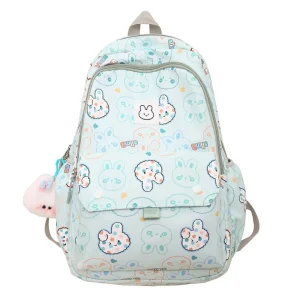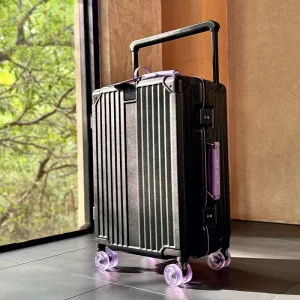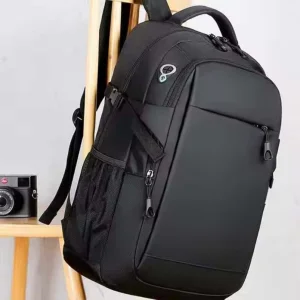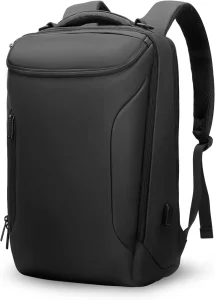
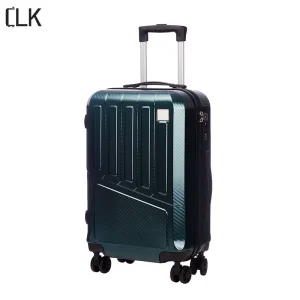
Dongguan ESRT Life Co., Ltd. stands as an established industry benchmark, operating as a professional manufacturer specializing in premier travel gear and lifestyle solutions. Positioned distinctively as a Luggage & Backpack Manufacturer | Durable Travel Bags & Business Travel Gear supplier, the enterprise integrates precision design, robust engineering, and consumer-centric functionality to service international markets efficiently.
Established in 2012 within the industrial powerhouse of Dongguan, China, ESRT Life originated as a dedicated workshop focused on foundational travel bags and fabric luggage tailored for domestic markets. Through continuous operational refinement and a forward-thinking strategic vision, the organization responded dynamically to the unprecedented expansion of global travel, e-commerce ecosystems, and urban outdoor lifestyles. Over successive years, the company scaled its operations into an expansive, vertically integrated product ecosystem encompassing rigid hard-shell suitcases, highly adaptive multifunctional backpacks, sophisticated business travel solutions, and rugged outdoor gear.
By 2017, ESRT Life achieved a major structural milestone by standardizing an elite manufacturing system. This upgrade incorporated advanced automated cutting machinery, high-precision digital sewing lines, stringent material innovations, and state-of-the-art ergonomic design laboratories. Today, the operational footprint is anchored by advanced production floors that guarantee uncompromising adherence to international quality management and environmental compliance frameworks.
Dongguan’s position as a premier global manufacturing hub provides ESRT Life with unmatched logistical and material access. Proximity to high-grade textile mills, zipper manufacturers, and hardware innovators ensures rapid prototyping, strict cost control, and consistent raw material integrity without compromising environmental standards.
Modern global consumers demand versatility. The convergence of remote work, bleisure travel (business + leisure), and urban commuting has accelerated the shift toward hybrid multi-purpose travel bags. Features such as integrated USB charging, RFID blocking pockets, and modular packing configurations are no longer luxury additions—they are baseline market expectations.
Our multi-purpose travel bags and luggage lines are engineered to perform flawlessly across diverse global environments, ranging from fast-paced corporate boardrooms in New York and Frankfurt to rugged outdoor trails in Scandinavia and crowded commuter transit networks across Southeast Asia.
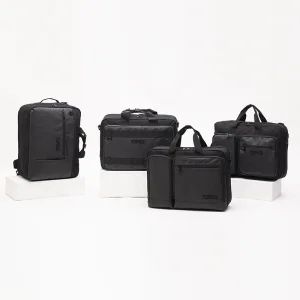
Tailored for corporate executives and frequent flyers requiring organized compartments for laptops, documents, and apparel, ensuring seamless airport security clearance and professional presentation.
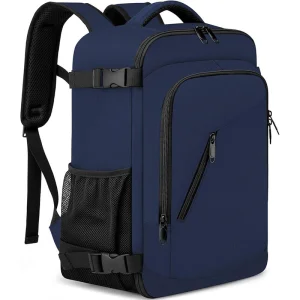
Designed to meet international airline overhead bin and underseat constraints (such as 20L cabin configurations), maximizing internal carrying capacity while maintaining lightweight ergonomics.
Crafted using high-tenacity, water-resistant nylon and reinforced stitching to withstand environmental stressors during weekend getaways, gym sessions, and outdoor excursions.
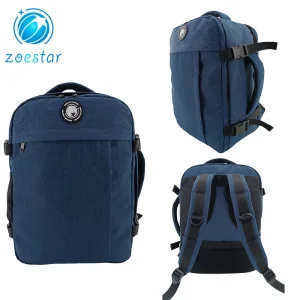
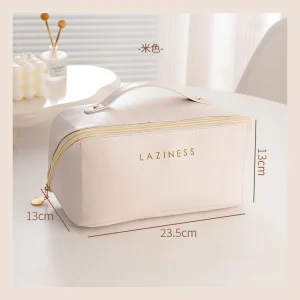
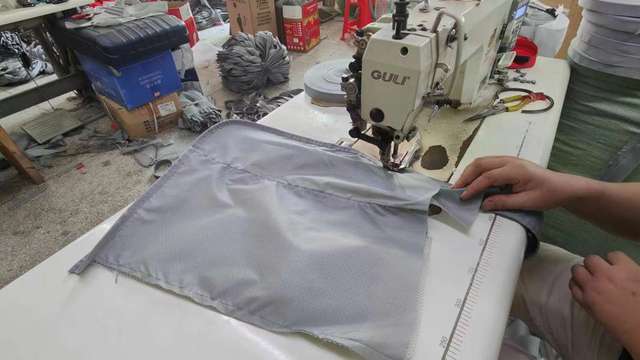
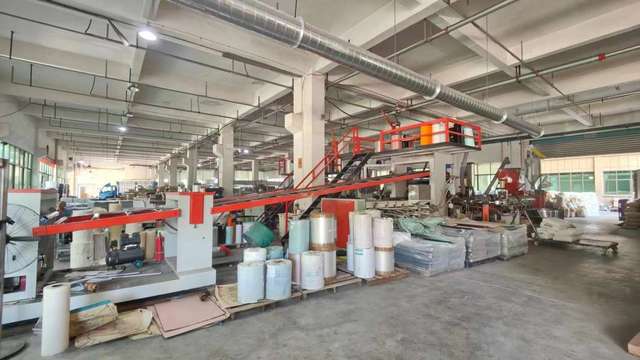
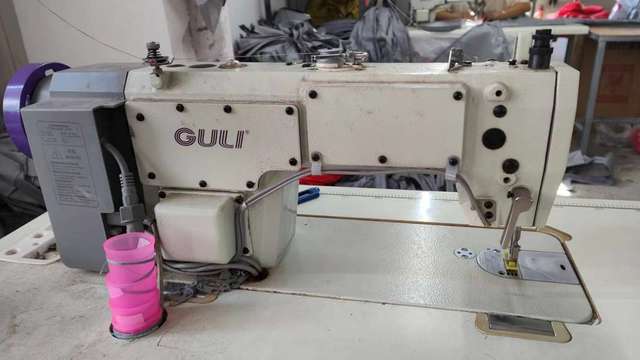
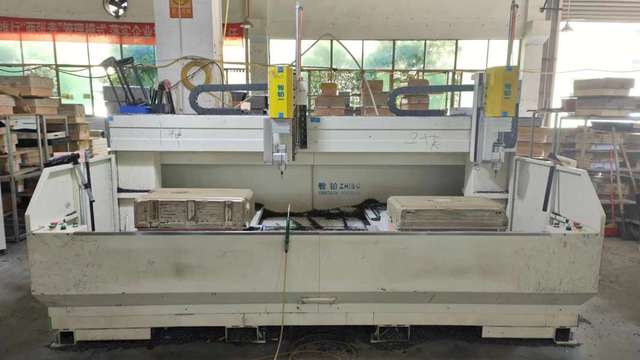
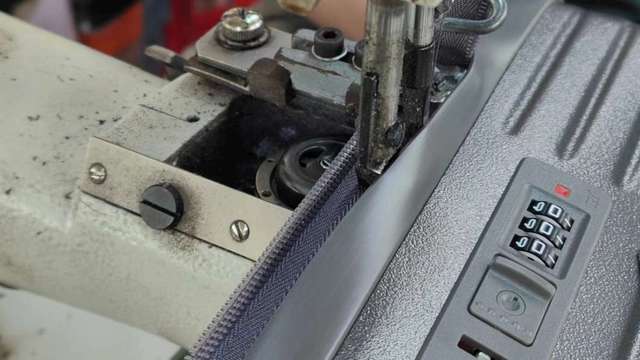
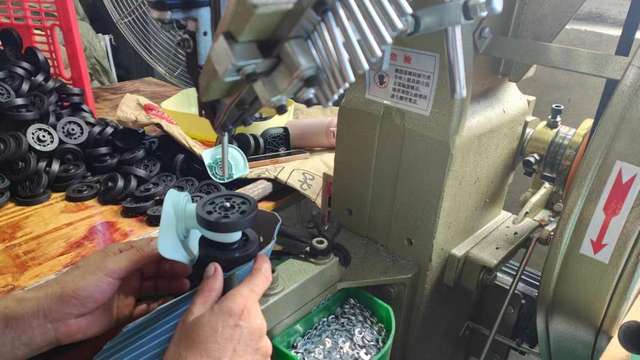
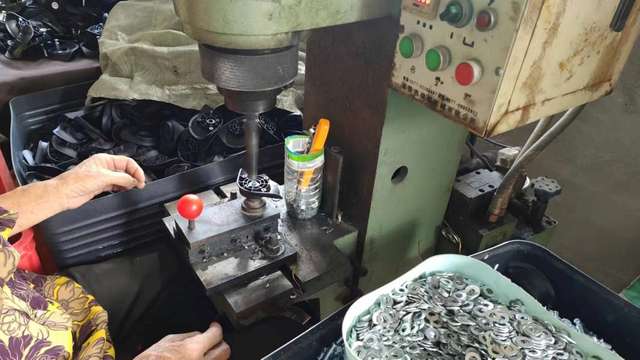
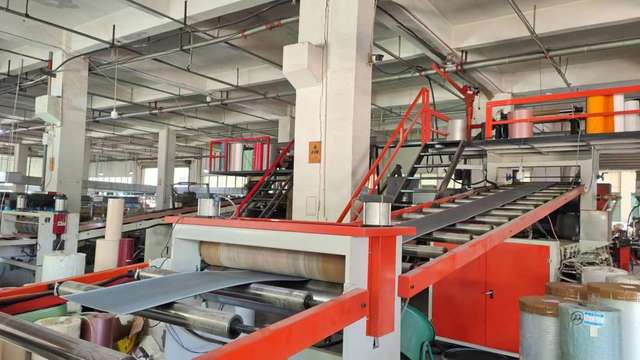
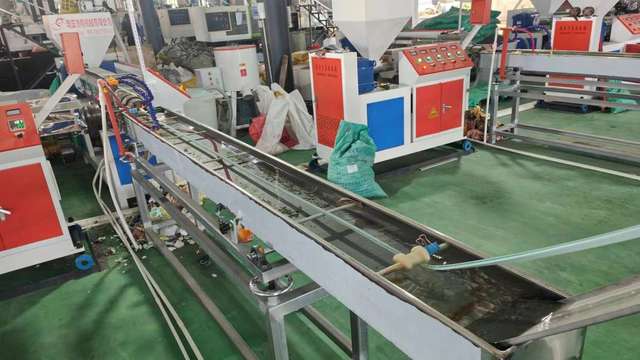
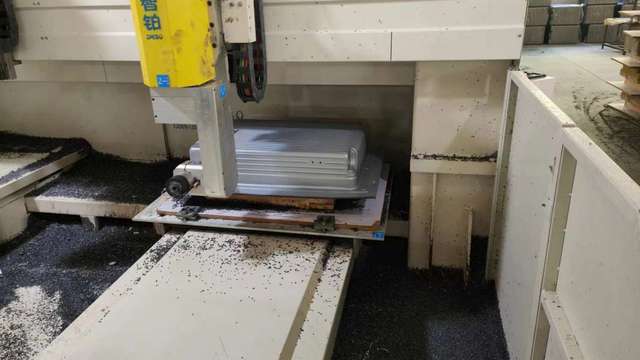
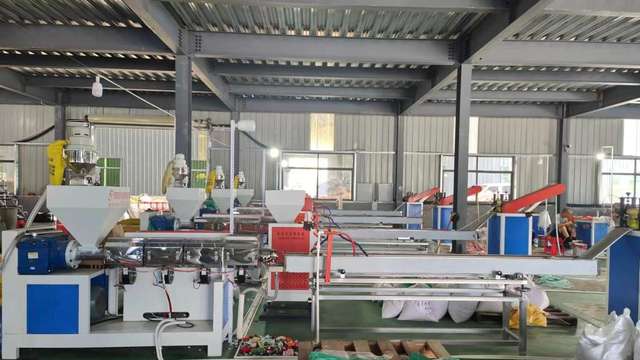
With over a decade of manufacturing expertise since 2012, we combine advanced automated production lines, rigorous E-E-A-T quality compliance, and responsive global supply chain management to deliver durable, stylish, and functional travel solutions tailored to international standards.
Yes, we specialize in comprehensive OEM and ODM partnerships. From custom branding, specialized fabric selection, and ergonomic structural modifications to smart integration like USB charging ports, our engineering team brings your precise product vision to life.
Our MOQ structures are designed to accommodate both emerging brand startups and large multinational distributors. Please reach out directly to our sales and engineering team with your specific project parameters for a tailored quotation.
Our manufacturing facilities operate under strict ISO and environmental guidelines. All travel bags undergo rigorous stress testing, waterproofing evaluations, zipper durability assessments, and seam strength testing before final dispatch.
 ESRT Life